Skip to content
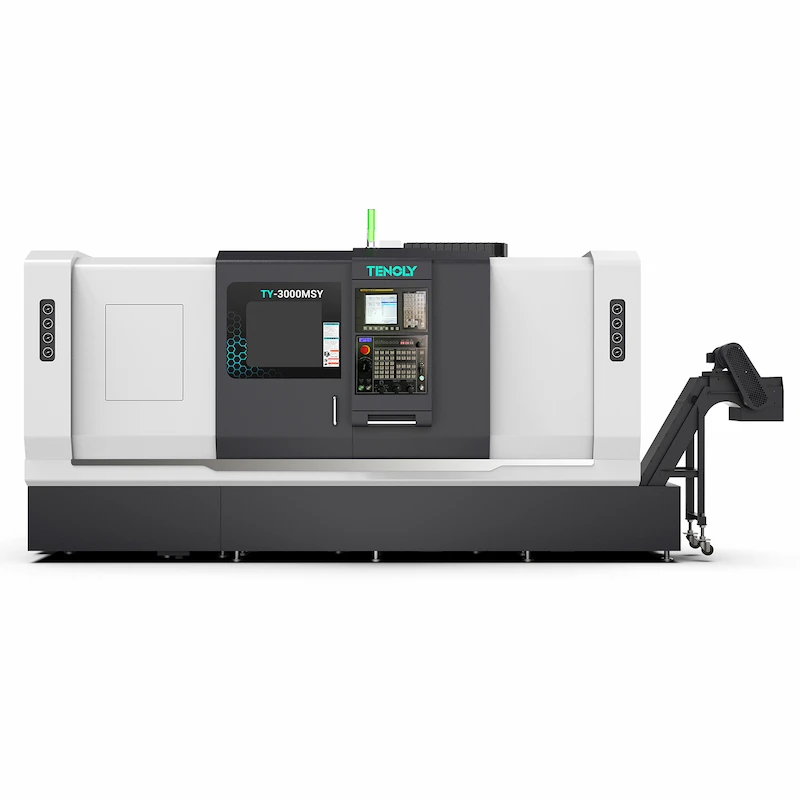
Roughing aims to quickly remove a large amount of material and form a blank, emphasizing processing efficiency and stability. Finishing, on the other hand, aims to achieve final dimensions, geometric accuracy, and surface quality, emphasizing high precision and surface finish.

| Project | Roughing | Finishing |
| Processing Objectives | Rapidly form blanks and remove large amounts of material as quickly as possible. | Achieving final dimensions, geometric accuracy, and surface quality. |
| Process Parameters | Deep turn, fast forward, low-speed stability. | Shallow turn, low feed, high speed. |
| Tool Selection | High rigidity, impact resistance, and ability to withstand large turning forces. | High precision, high wear resistance, and sharper turning edge. |
| Coolant Use | Primarily focused on cooling and lubrication to reduce temperature and minimize wear. | Rust prevention, cleaning, and lubrication should be given equal importance to improve surface integrity. |
| Machining Allowance | A relatively large allowance, typically ranging from a few millimeters to over ten millimeters. | Small margin, typically between a few tenths of a millimeter and a few millimeters. |
| Surface Quality Requirements | Relatively low, with tool marks and machining traces present. | High quality, low defects, surface Ra reaches the micrometer level or even smaller. |
| Machining Efficiency | High efficiency and rapid material removal. | Aiming for high precision, the time required is relatively long. |
1. Processing Objectives
The core objective of roughing is to quickly remove excess material from the workpiece, making it close to the final product in shape and size, providing a suitable blank for subsequent finishing. High processing efficiency is used to minimize processing time, ensuring production cycle time and cost control. In contrast, finishing focuses on achieving final dimensional accuracy, geometric tolerances, and surface quality, meeting the stringent requirements of design intent and performance. Both represent a progressive process from rapid material removal to high-precision surface improvement, a crucial step in achieving a balance between part quality and production efficiency.
2. Process Parameters
In the roughing stage, a combination of large depth of cut, high feed rate, and low turning speed is typically used. This parameter configuration helps to quickly remove a large amount of material while improving productivity through higher turning forces and turning volume. The toolpath primarily focuses on contour approximation and rough contour removal, emphasizing stability and efficiency. The finishing stage tends towards smaller depths of cut and feed rates, while increasing the CNC lathe’s turning speed to reduce turning forces, minimize deformation risk, and achieve a more stable machining process and higher surface quality. High-precision geometric control and smaller machining errors become the core objectives of this stage, ensuring the final dimensions meet tolerance requirements.
3. Tool Selection
Roughing typically uses high-strength, rigid, and impact-resistant tools, such as carbide tools and ceramic tools, to withstand greater turning forces and impacts, ensuring efficient material removal without damage. Finishing favors high-precision, high-wear-resistant tools, such as diamond tools and cubic boron nitride tools. These tools achieve extremely high surface quality and dimensional consistency with sharper turning edges and more stable geometric characteristics. The tool selection in both stages reflects the trade-off between material removal efficiency and surface control.
4. Coolant Use
The coolant used in the roughing stage primarily serves cooling and lubrication, reducing turning temperature, minimizing tool wear, and improving stability and machining safety. Generally, emulsions or water-soluble coolants with good cooling properties are preferred, balancing cost and performance. In the finishing stage, in addition to cooling and lubrication, good rust prevention, cleaning, and lubrication properties are required to protect the workpiece surface from oxidation and ensure stable surface quality. Turning oils or extreme pressure coolants with lower viscosity and better lubricity are generally selected to achieve lower CNC machine turning heat and better surface integrity.
5. Machining Allowance
Roughing typically leaves a large machining allowance, ranging from a few millimeters to tens of millimeters, to ensure sufficient material for final machining, error correction, and shape finishing. Finishing has a smaller machining allowance, usually between a few tenths of a millimeter and a few millimeters, mainly used to remove machining marks and trace amounts of material left from roughing, and to achieve higher dimensional stability and surface quality. Proper allocation of the machining allowance is a crucial prerequisite for achieving final tolerances and surface quality.
6. Surface Quality Requirements
Roughing has lower surface quality requirements; surface roughness Ra is often between tens and hundreds of micrometers, and obvious tool marks and machining traces may be present. This prioritizes improving machining efficiency and the ability to remove roughness. Finishing demands extremely high surface quality; Ra can be several micrometers or even smaller. The workpiece surface should be smooth, flat, and free of obvious tool marks and defects to meet performance, assembly fit, and aesthetic requirements. Differences in surface quality directly affect subsequent assembly, fatigue life, and functional performance.
7. Machining Efficiency
Roughing emphasizes machining efficiency, utilizing larger turning parameters and high feed rates to remove large amounts of material in a short time, thereby shortening the machining cycle. Finishing, on the other hand, focuses on stability and precision. Although turning parameters are relatively conservative and machining time is usually longer, high-quality turning tools and optimized processes can achieve extremely high dimensional accuracy and surface quality, thus ensuring the reliability and lifespan of critical components.
Summary
· Roughing and finishing are two key steps in achieving efficient and high-precision manufacturing, each with different objectives and technological requirements.
· In actual production, a progressive process route is typically adopted, first performing roughing to achieve rapid blank formation, and then performing finishing to meet the final technical requirements.
· The proper coordination of process parameters, turning tools, coolant, and machining allowances is crucial to ensuring machining stability, dimensional accuracy, and surface quality.